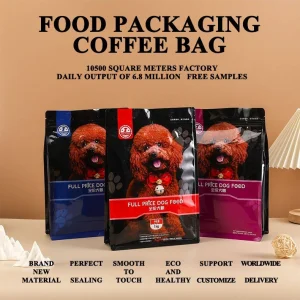
The global cellophane packaging market has undergone a significant transformation over the last decade. Once viewed as a traditional material, cellophane has seen a resurgence as a premium, biodegradable alternative to petroleum-based plastics. Today, the industry is valued at billions of dollars, driven by the global push for sustainability and the unique barrier properties that cellophane provides. As a leading cellophane packaging factory, we have observed a sharp increase in demand from sectors such as organic food, luxury cosmetics, and pharmaceutical industries.
In the current industrial landscape, European and North American markets are leading the regulation of single-use plastics, creating a vacuum that high-quality, plant-based films are filling. Cellophane, derived from natural cellulose, offers the perfect combination of transparency, high-heat resistance, and compostability. This makes it a top choice for brands aiming to reduce their carbon footprint while maintaining shelf-life integrity.
The shift towards 100% compostable and recyclable materials is no longer a niche; it is a global mandate. Our factory integrates bio-based resins to enhance film performance.
Integration of QR codes and RFID for traceability. AI-driven quality control in our production lines ensures zero-defect manufacturing for high-stakes industries.
New technologies allow us to apply ultra-thin barrier layers to cellophane, rivaling the oxygen and moisture protection of traditional aluminum foils.
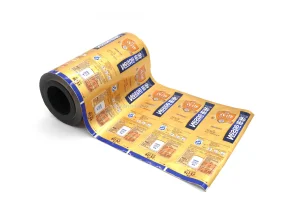
Our Customized Milk Powder Packaging Film represents the pinnacle of multi-layer extrusion technology. Designed for sensitive food products, it offers an impenetrable shield against UV light, oxygen, and moisture.
Utilizing high-grade polymers and specialized foils, this product ensures the nutritional integrity of powdered supplements and dairy products for extended shelf lives in diverse climates.
Global procurement managers are increasingly looking to China not just for cost-efficiency, but for integrated supply chain excellence. As a premier cellophane packaging exporter, Tongcheng Packaging Materials Co., Ltd. provides a one-stop solution from raw material blowing to intricate gravure printing. The speed of innovation in China allows factories to prototype and scale new packaging formats faster than anywhere else in the world.
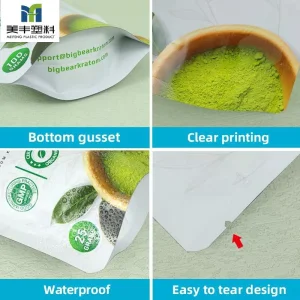
In the fast-paced world of beverage retail, our Matcha Coffee Sachet Packaging is a market leader. It combines aesthetic appeal with functional durability.
These pouches are engineered for high-speed filling lines, featuring easy-tear notches and customizable matte or glossy finishes that resonate with modern consumers' preferences for premium design.
Since 1985, Tongcheng Packaging Materials Co., Ltd. is a senior professional manufacturer in supplying flexible packaging by international standards. Our products exported to countries in Europe, America and Southeast Asia. The company covers a total area of 5500 square meters and has 7700 square meters for building. The company's registered capital is RMB 11.98 million Yuan. There are totally 150 lovely employees working together. Equipped with gravure plate making, printing, lamination, slitting, bag-making and film-blowing and testing areas, our annual production capacity reached 5000 tons.
We follow quality control system of ISO22000 and GB 9683-1988 strictly to ensure quality. Based on this, our products are exported to clients all over the world. All these products are qualified after being tested by authentic system.
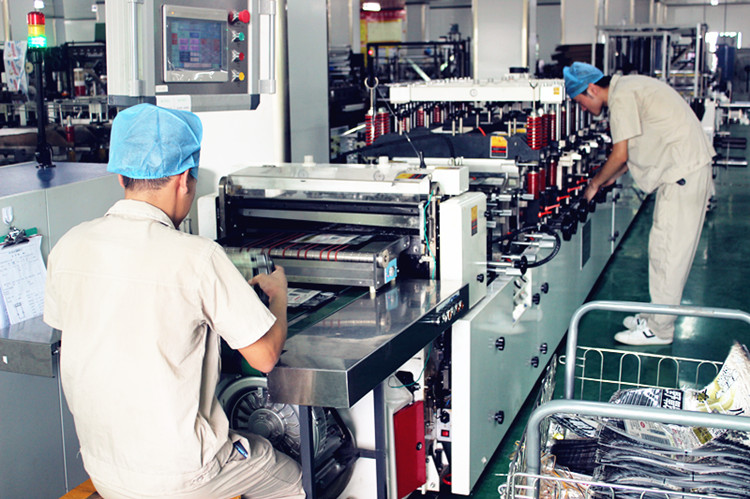
Advanced Production Equipment: Our facility is equipped with state-of-the-art machinery that allows for precision printing and high-strength lamination, ensuring that every roll of film and every bag produced meets the highest industry benchmarks.
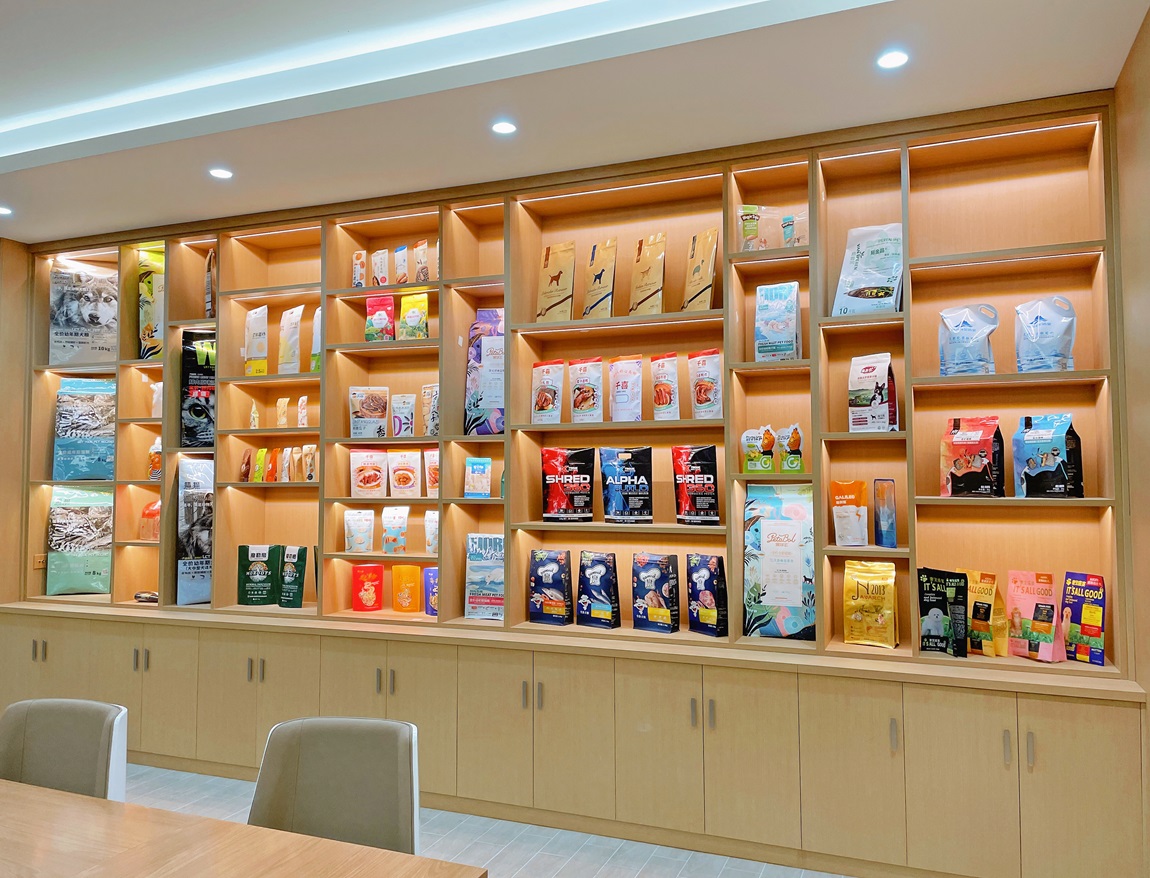
Cellophane and flexible packaging applications vary significantly across regions. In Southeast Asia, the focus is heavily on individual sachets for coffee and snacks due to the "sachet economy." In Europe, the demand is pivoted toward "Eco-friendly" and "Recyclable" certifications for gourmet food wrapping. Meanwhile, in North America, the rise of e-commerce has increased the demand for rigid subscription boxes and protective tubes.
 Premir Plastic Package